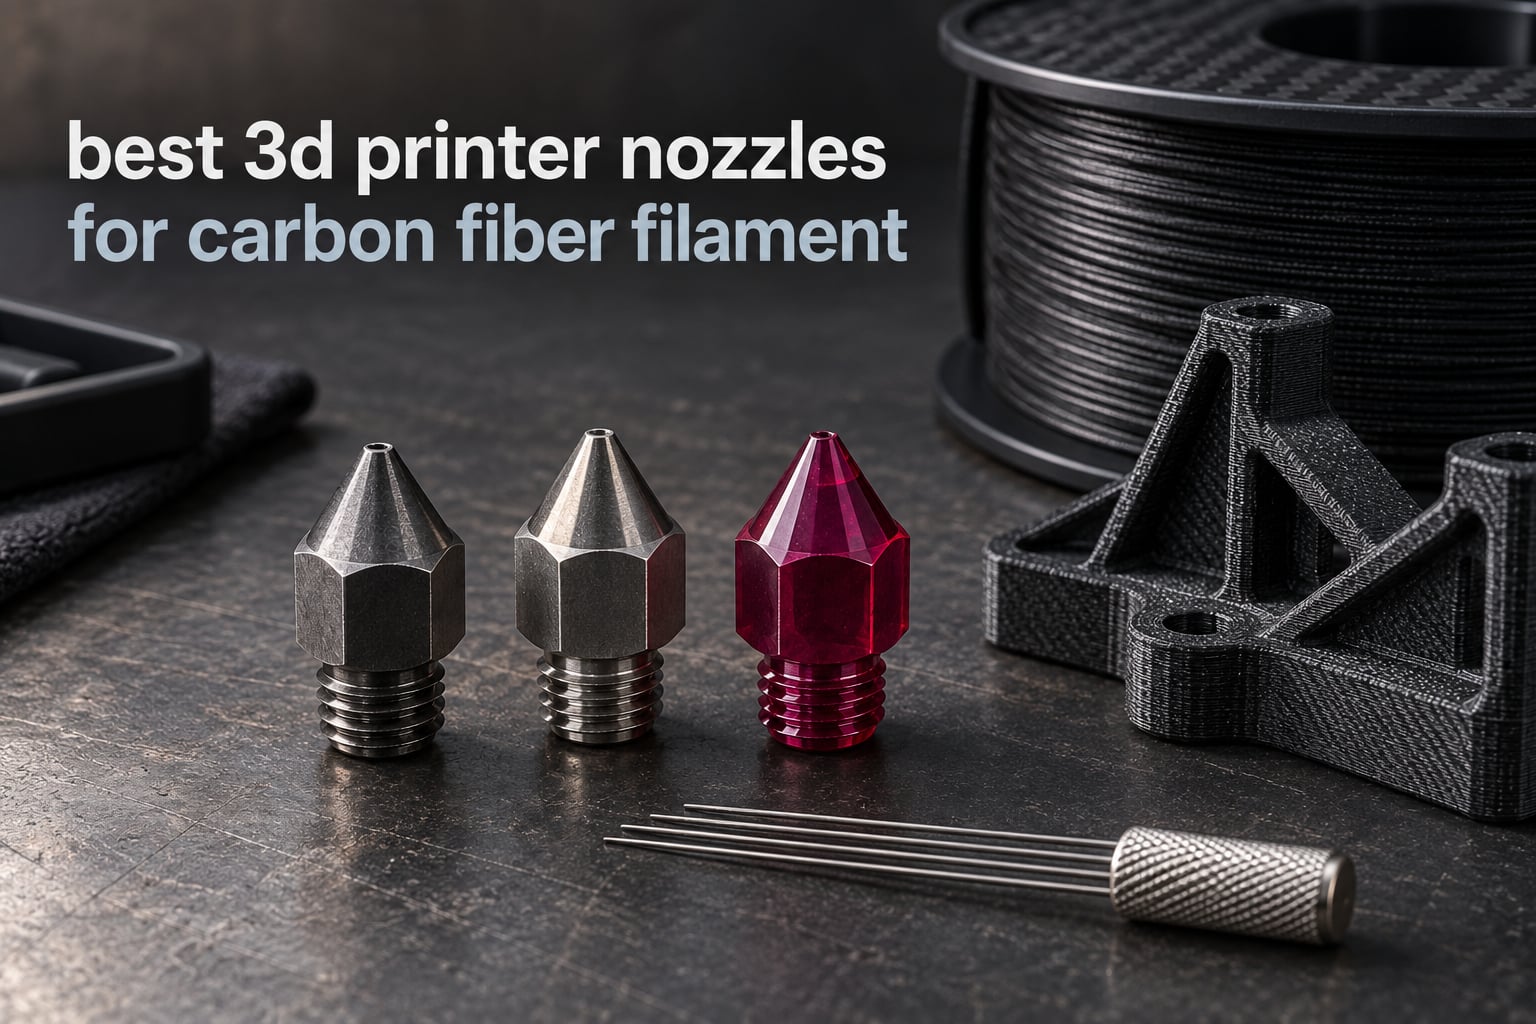
Brass nozzles cannot be trusted with carbon fiber filament. Chopped carbon strands act like sandpaper against the orifice at melt temperature, and a brass hole widens within a few prints, which shows up as over-extrusion, stringing and parts that no longer fit. For occasional PLA-CF or PETG-CF work, a hardened steel nozzle is enough. For regular PA-CF, PA6-CF or PPA-CF printing, step up to tungsten carbide or a ruby tip in a copper-alloy body.
That is the short version. The long version is that the best 3d printer nozzles for carbon fiber filament are not ranked by hardness alone. Thermal conductivity decides whether your melt zone keeps up, bore quality decides whether you fight clogs, and the thread standard decides whether the nozzle fits your printer at all. Get any of those three wrong and the money you spent on a premium tip is wasted.
We compared twelve nozzles built for abrasive filament, spanning MK8 screw-in, V6/M6, Bambu quick-swap, Creality Spider, and QIDI and Flashforge chute-fit formats. Nine are hardened steel, one is tungsten carbide, and three use genuine ruby tips. For each one we looked at the material spec, the fitment, the bore geometry, and what owners actually reported after months of filament rather than a few test prints.
Our top pick is the Mudder hardened steel 0.4 mm MK8 10-pack, because it has the deepest owner history in the group and a bore that stays round under load. If you run a Bambu machine, the OEM hardened hotend is the cleanest path. If you print engineering-grade nylon daily, the tungsten carbide and ruby options at the bottom of this guide are the ones that pay for themselves.
Table of Contents
Top 3 Picks: Best 3d Printer Nozzles For Carbon Fiber Filament (October 2026)

Mudder Hardened Steel 0.4 mm MK8 10-Pack
- Hardened tool steel
- 10-nozzle pack
- Burr-free CNC bore
- Under 0.02 mm diameter error
- Fits MK8 hotends

Bambu Lab Hardened Steel Hotend 0.4 mm
- Official OEM hotend assembly
- 0.4 mm hardened steel
- 300°C maximum
- For X1C P1P and P1S

HzdaDeve Hardened Steel Kit for Bambu A1
- Hardened steel hotend kit
- Up to 350°C
- Quick-swap for A1 A1 mini A2L
- Removable tip only
All 12 Nozzles Compared Side by Side in 2026
| Product | Specifications | Action |
|---|---|---|
| Mudder Hardened Steel 0.4 mm MK8 10-Pack |
|
Check Latest Price |
| HzdaDeve Hardened Steel Kit for Bambu Lab A1 |
|
Check Latest Price |
 POLISI3D Hardened Steel V6 0.4 mm 4-Pack |
|
Check Latest Price |
| Bambu Lab OEM Hardened Steel Hotend 0.4 mm |
|
Check Latest Price |
 Flashforge Adventurer 5M Pro Hardened 0.6 mm |
|
Check Latest Price |
 Micro Swiss Plated Wear Resistant V6 0.4 mm |
|
Check Latest Price |
 LANKEGU Hardened Steel 0.4 mm Kobra 2 6-Pack |
|
Check Latest Price |
 POLISI3D Spider Hotend Hardened 0.4 mm 2-Pack |
|
Check Latest Price |
 Dawnblade Tungsten Carbide MK8 0.4 mm |
|
Check Latest Price |
 DUROZZLE Ruby 0.8 mm for QIDI Q1-Pro |
|
Check Latest Price |
 DUROZZLE Ruby 0.8 mm for Flashforge AD5X |
|
Check Latest Price |
 DUROZZLE Quick-Swap Ruby 0.4 mm for Creality K2 |
|
Check Latest Price |
What nozzle do you need for carbon fiber filament?
Use a hardened steel nozzle for PLA-CF and PETG-CF if you print them occasionally, a tungsten carbide nozzle if you run PA-CF regularly, and a ruby nozzle in a copper-alloy body if carbon fiber is a daily material on your machine. Brass is not a realistic option for abrasive filament beyond a single print.
The reason is physical. Every carbon fiber strand in the filament is a hard cylinder being dragged through a hardened hole at extruder temperature, and the hole is the only surface in the path. As the orifice widens, the flow area grows, more material comes out than the firmware commands, and the layer lines thicken. That is why worn nozzles produce blobs, stringing and walls that drift out of tolerance even though every slicer setting is correct.
There is a second surprise that catches people out. Hardened steel moves heat badly compared with brass, so the melt zone inside the nozzle runs cooler than the number on the heater block display. A print that was fine on brass can underextrude badly on a steel tip until you add temperature. Budget 5 to 15 degrees for the first adjustment, then re-tune PID, because the controller is now working with a very different thermal mass.
Forum threads ask constantly whether to own two nozzles or swap one. Both work. The two-nozzle route keeps a clean brass tip for PLA and PETG so carbon fiber residue never blobs on a print you care about, and it saves you a swap every time you change material. The single-nozzle route costs less and is fine if you run a cold pull or two between materials.
The same threads raise the durability question, and the honest answer is that both the pessimistic and optimistic reports are partly right. Vendors quote brass lasting only tens of hours on PA-CF, and a number of owners on r/3Dprinting report pushing a full roll of carbon fiber blend through a brass nozzle on an Ender 3 without noticing damage. Both can be true, because a short cool-tower print barely touches the melt zone while a long hot print parks molten nylon against the orifice for hours.
If you want a general primer on fiber-reinforced material and the tools around it, our guides to fiber laser engravers and the history of fiber art cover the wider world of fiber reinforcement. For the nozzle itself, the rule is simple: match hardness to how much carbon fiber you push through it per month.
How we picked the best nozzles for carbon fiber filament
Four criteria decided the order, and each one reflects a way a nozzle purchase actually goes wrong. First is fitment, because an incompatible thread is a wasted purchase no matter how good the tip is. Second is bore quality, since a rough internal channel is the single most common cause of clogs attributed wrongly to the filament.
Third is owner-reported durability. Where written reviews existed, we weighted repeated use over first impressions. Where the data returned no written review text, we say so plainly and lean on the manufacturer spec instead of pretending to have evidence. Fourth is thermal behaviour, because a nozzle that cannot hold melt temperature in a long print will undercut every durability advantage it offers.
We did not run a controlled wear test. Every lifespan figure in this guide comes from the material spec, the filament type, or what owners reported, and we have attributed each one rather than blending them into a single invented number. Where a claim is unverified, it is labelled as unverified.
1. Mudder Hardened Steel 0.4 mm MK8 10-Pack – the one most Ender owners start with
- Deepest owner history in the group at more than 2000 reviews
- Holds up across multiple kilograms of carbon-PLA and glow filament
- Consistent 0.4 mm bore checked with a needle gauge
- Ten tips means spares are always on the shelf
- Two-flat body instead of a full hex so a socket wrench will not fit
- A small group report clogs that temperature changes did not fix
- Steel tips are not flat on all sides so pliers need care
This is the pack we keep coming back to, and the reason is boring rather than exciting. More than two thousand owners have run it, which means the failure modes are well known, and the known failure modes are minor. The two-flat body instead of a hex will not accept a socket wrench, and the steel tip is not ground flat on every face, so both details cost you thirty seconds during installation.
The bore is the part that matters. Owners checking with a needle gauge report a consistent 0.4 mm opening, and the stated diameter error of under 0.02 mm is consistent with what people see under magnification. That is the difference between a nozzle that feeds smoothly and one that repeatedly catches on a fiber bundle and stalls.
Compatibility is the reason this is first. The MK8 screw-in thread covers the Ender 2, 3, 3 Pro and 5, the CR-10 all-metal hotend, the Prusa i3, the Anet A8 and Reprap machines generally. That is the widest footprint of any hardened nozzle in this guide, and the ten-piece pack means the spares cost almost nothing relative to the outlay.
It ships in a pack of ten, weighs under an ounce per tip, and measures 4.29 by 2.83 by 0.63 inches for the whole pack. Owners using it for carbon-PLA, glow-in-the-dark PLA and standard PLA report consistent extrusion across long abrasive jobs with no clogging, and it drops straight into a stock Ender hotend without temperature changes to the profile.
Who should buy the Mudder MK8 pack
Buy it if you run an Ender, a CR-10 or a Prusa i3 on the MK8 standard and you print carbon fiber occasionally. It is also the sensible first upgrade for anyone whose only current option is the brass nozzle that came with the printer, because ten tips make a mistake cheap.
It is a strong choice for PETG-CF and PLA-CF specifically, where the abrasive load is lower than it is in PA-CF. Ten spare tips in a drawer is the practical argument. You will burn through one eventually, and when you do you do not want to stop mid-project to order a replacement.
Who should skip it
Skip it if you run PA-CF or PPA-CF every day. Steel is the right entry point, not a long-term answer for high-temperature nylon loaded with fiber, and the cost difference per hour works against you over thousands of print hours.
Also skip it if you need a hex body and enjoy the convenience of a wrench, or if you have a V6, MK10, Bambu, Creality Spider, QIDI or Flashforge machine. The thread is wrong for all of those, and a wrong thread means the nozzle will not seat.
2. HzdaDeve Hardened Steel Kit for Bambu Lab A1 – best value for quick-swap Bambu
2 Pack 0.4mm A1 Mini/A1/A2L Hotend Kit Hardened Steel Nozzle for Bambu Lab
- Plug-and-play with no tools or printer modification
- Reported layer lines match the original Bambu nozzle
- Removable tip means you swap the nozzle not the hotend
- Includes a silicone nozzle sock
- A few buyers hit first-day jamming and metal flakes
- The holding magnet fell out on one assembly
- Some arrived needing thorough cleaning before running
This is the option that makes an A1 or A1 mini print carbon fiber without a teardown. The nozzle is threaded into the hotend assembly rather than bonded in, so a worn tip is a short swap rather than a new extruder. At 350°C rated operation it also covers the PA and PC blends that the stock hotend struggles with.
Owners report print accuracy and layer lines that match the original Bambu nozzle, which matters more than it sounds. A nozzle that changes your wall thickness or your first-layer height is not a drop-in upgrade, it is a recalibration project. This one largely avoided that complaint across most of its reviews.
The quality picture is not perfect, and we would rather say so. A small number of buyers reported jamming in the first hours of use along with metal flakes that pointed at internal fit rather than filament, and a few found the assembly needed real cleaning before it would feed. The silicone sock in the box is a nice touch that most people forget to install on a replacement hotend.
Weighing 2.39 ounces and measuring 4.69 by 3.78 by 1.02 inches, this is a compact assembly that adds nothing to the machine profile. The stated durability claim of five to ten times a standard brass nozzle is a manufacturer figure we cannot verify independently, but the owner reports of clean PLA-CF and PETG-CF output are consistent with hardened steel doing its job.
Who should buy the HzdaDeve Bambu kit
Buy it if you own an A1, an A1 mini or an A2L and you want carbon fiber capability on a budget without replacing the whole hotend. It is the best value in this guide for that specific group because the quick-swap design removes the usual upgrade friction.
It also suits a first carbon fiber print on a Bambu machine, where the priority is a reliable tip in the right thread at a sane outlay rather than the longest possible service life. Owners moving from the factory tip report a marked improvement on abrasive materials.
Who should skip it
Skip it if you print nylon loaded with fiber daily, because a hardened steel tip is an entry solution and the ruby and carbide options hold up far better at temperature. Skip it if you own a P1S, P1P or X1C instead, since this kit is built for the A1 family and A2L.
If quality control on the first arrival matters to you, inspect the tip under magnification before installing. The jamming reports are a minority, but they cluster in the first hours, which means they are cheap to catch early and expensive to discover mid-print.
3. POLISI3D Hardened Steel V6 0.4 mm 4-Pack – best fit for Prusa and E3D V6 hotends
- Prints carbon fiber nylon alongside PETG and PLA
- Shows less heat jamming than brass on high-flow hotends
- Hex flats do not deform when tightened
- Long-running listing with consistent owner reports
- Size is marked with dots not printed numerals
- Can sit slightly shorter than the factory part
- Z-offset may need a small correction
The V6 and M6 thread is the most common high-performance thread in the hobby, and this set covers the machines that use it: Prusa i3 MK3 and MK3S, the Prusa Mini, and the Anycubic Mega. If your hotend is an E3D V6 derivative, this is the format to buy, and the four-pack means you have a spare for a wear test comparison.
Owners specifically report less heat-jamming tendency than brass on high-flow hotends, which is the less obvious benefit of hardened steel. Steel takes longer to reach temperature and holds it more steadily, and on a hotend that struggles with sudden flow demands that stability prevents the partial jams that brass invites. The hex flats also survive tightening without deforming, so the nozzle keeps seating properly.
Two practical details catch people. The size is indicated by the number of dots on the tip rather than printed numerals, which is easy to misread when you are reaching for a specific diameter in a hurry. And the nozzles can measure slightly shorter than the factory part, so expect to touch up Z-offset after installation rather than treating it as a fault.
It is CNC machined, comes in a four-piece 0.4 mm set for 1.75 mm filament, and is rated for PEI, PEEK and carbon fiber. A multi-size variant covering 0.25, 0.4, 0.5 and 0.6 mm also exists, which matters if you plan to move to a wider bore for particle-filled filament later.
Who should buy the POLISI3D V6 set
Buy it if your printer runs a V6 or M6 hotend, which covers a large share of Prusa i3 MK3-series, Prusa Mini and Anycubic Mega machines. It is a solid first upgrade over a brass V6 tip for anyone moving into PETG-CF or PA-CF part-time.
The four-pack is the reason to prefer it over a single nozzle. You can run one, keep one as a spare, and put a third through a filament changeover test to see whether the temperature offset needs a different value for your setup.
Who should skip it
Skip it if you run MK8, MK10, Bambu, Creality Spider or any chute-fed printer, since the thread will not match. Skip it if you print PPA-CF or PC-CF in production, where a carbide or ruby tip will outlast several of these.
One owner reported rust forming inside the nozzle and questioned whether the steel is genuinely hardened, and another order arrived with three nozzles and production scraps instead of four. Neither is common, but both are reasons to check the bore and the count on arrival.
4. Bambu Lab OEM Hardened Steel Hotend 0.4 mm – the cleanest fit for X1C and P1S
Genuine Bambu Lab Hotend with Nozzle for P1S P1P X1C X1 Carbon 3D Printer .4mm Hardened Steel
- Highest average rating in the guide at 4.6
- Reports clean carbon fiber nylon output
- Includes thermal grease and step screws
- Installation is straightforward with no adaptation
- One buyer reports it does not fit the X1C as listed
- One arrived in a crushed box looking used
- A suspected defect appeared on a second print
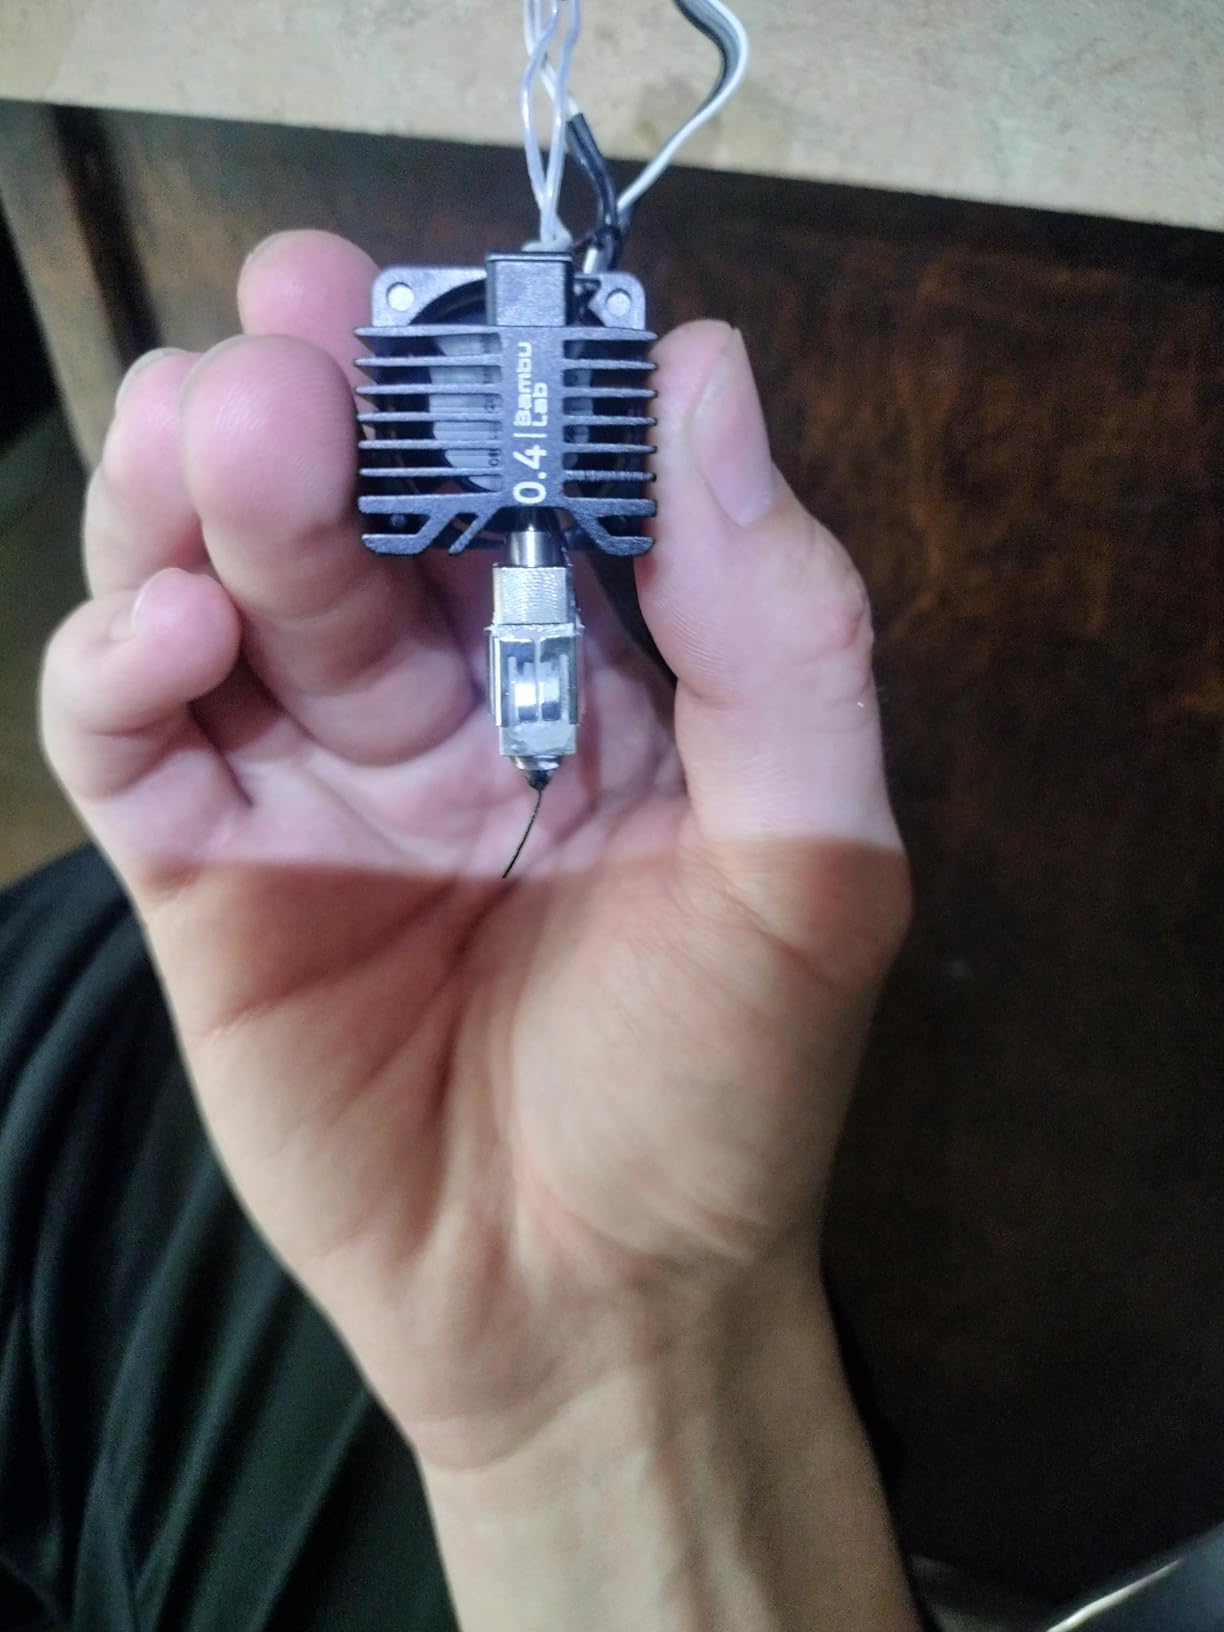
This is the one we recommend when you want zero ambiguity about fitment. It is the manufacturer’s own hotend assembly with a 0.4 mm hardened steel nozzle, supplied with a silicone sock, thermal grease for the heatsink and sensor, and M3-14 step screws. Nothing needs adapting, and nothing needs guessing.
It carries the strongest rating profile in the guide at 4.6 from 208 reviews with an 88 percent five-star share. Owners report printing carbon fiber nylon smoothly and, notably, clearing partial clogs that survived other cleaning attempts, which suggests the bore finish holds up under residue better than most aftermarket steel.
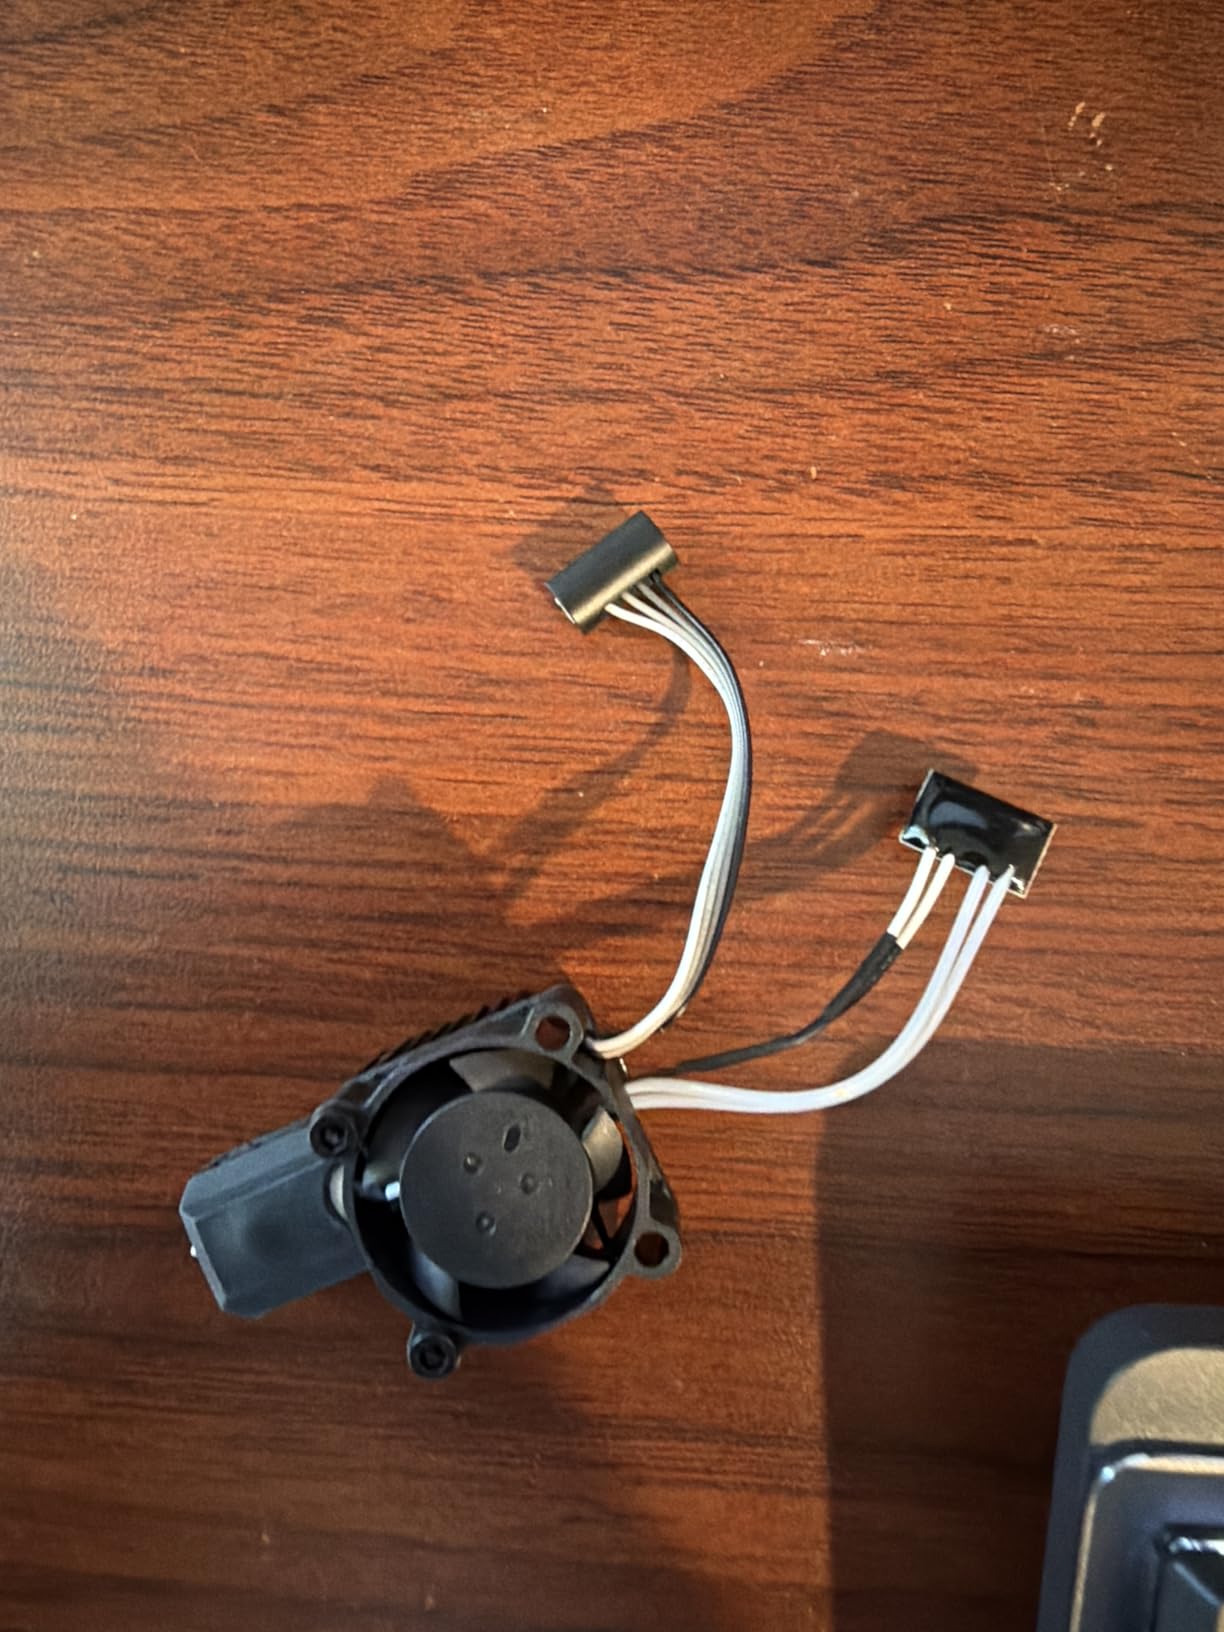
The 300°C maximum printing temperature is the specification to note. It comfortably covers PLA-CF, PETG-CF and most PA-CF blends, but it will not run PEEK-class material, and for PC-CF you are near the ceiling rather than comfortably inside it. The assembly weighs 1.06 ounces and measures 6.5 by 3.62 by 1.73 inches.
Owners also mention that the packaging looks identical to units bought direct from the manufacturer, which matters if you care about provenance. Thermal grease in the box saves a step, and on a hotend assembly the grease at the sensor mount is the difference between a stable reading and temperature drift that ruins layer adhesion.
Who should buy the Bambu OEM hotend
Buy it if you own a P1S, a P1P or an X1C and you want carbon fiber capability with an official part. For people who already trust the rest of the machine, the certainty is worth more than the small saving an aftermarket option would give.
It is also a good choice if you are not confident about the after-market supply chain for your printer. The rated 300°C ceiling covers the overwhelming majority of carbon fiber filaments people actually print at home.
Who should skip it
Skip it if you want higher temperature capability than 300°C or if you print PEEK and PEI regularly, because the rating will hold you back. Skip it if you run an A1, A1 mini or A2L, since this assembly is for the P1 and X1C generation.
Two caveats worth stating. One buyer reported that the assembly is for P1P and P1S and does not fit the X1C despite the listing title, so confirm your exact model before ordering. Another reported a suspected manufacturing defect on the second print, and the assembly does not include replacement wiring, which makes a failed hotend a bigger setback than a failed tip.
5. Flashforge Adventurer 5M Pro Hardened 0.6 mm – best for high-flow abrasive work
- Owners report several kilograms of PA6-CF on one tip
- Tool-free removal in about three seconds
- Cuts print times noticeably versus smaller bores
- Clear gain over the factory brass tip
- One buyer smashed the nozzle into the build plate
- Some report the tip dying after a couple of months
- Clog complaints trace back to incompletely dried filament
This is the pick if you care about throughput more than detail. A 0.6 mm bore moves roughly twice the material per second of a 0.4 mm, and with a stated 32 mm3/s maximum flow the hotend is designed to keep feeding it during long abrasive prints where a small bore would spend most of its time waiting.
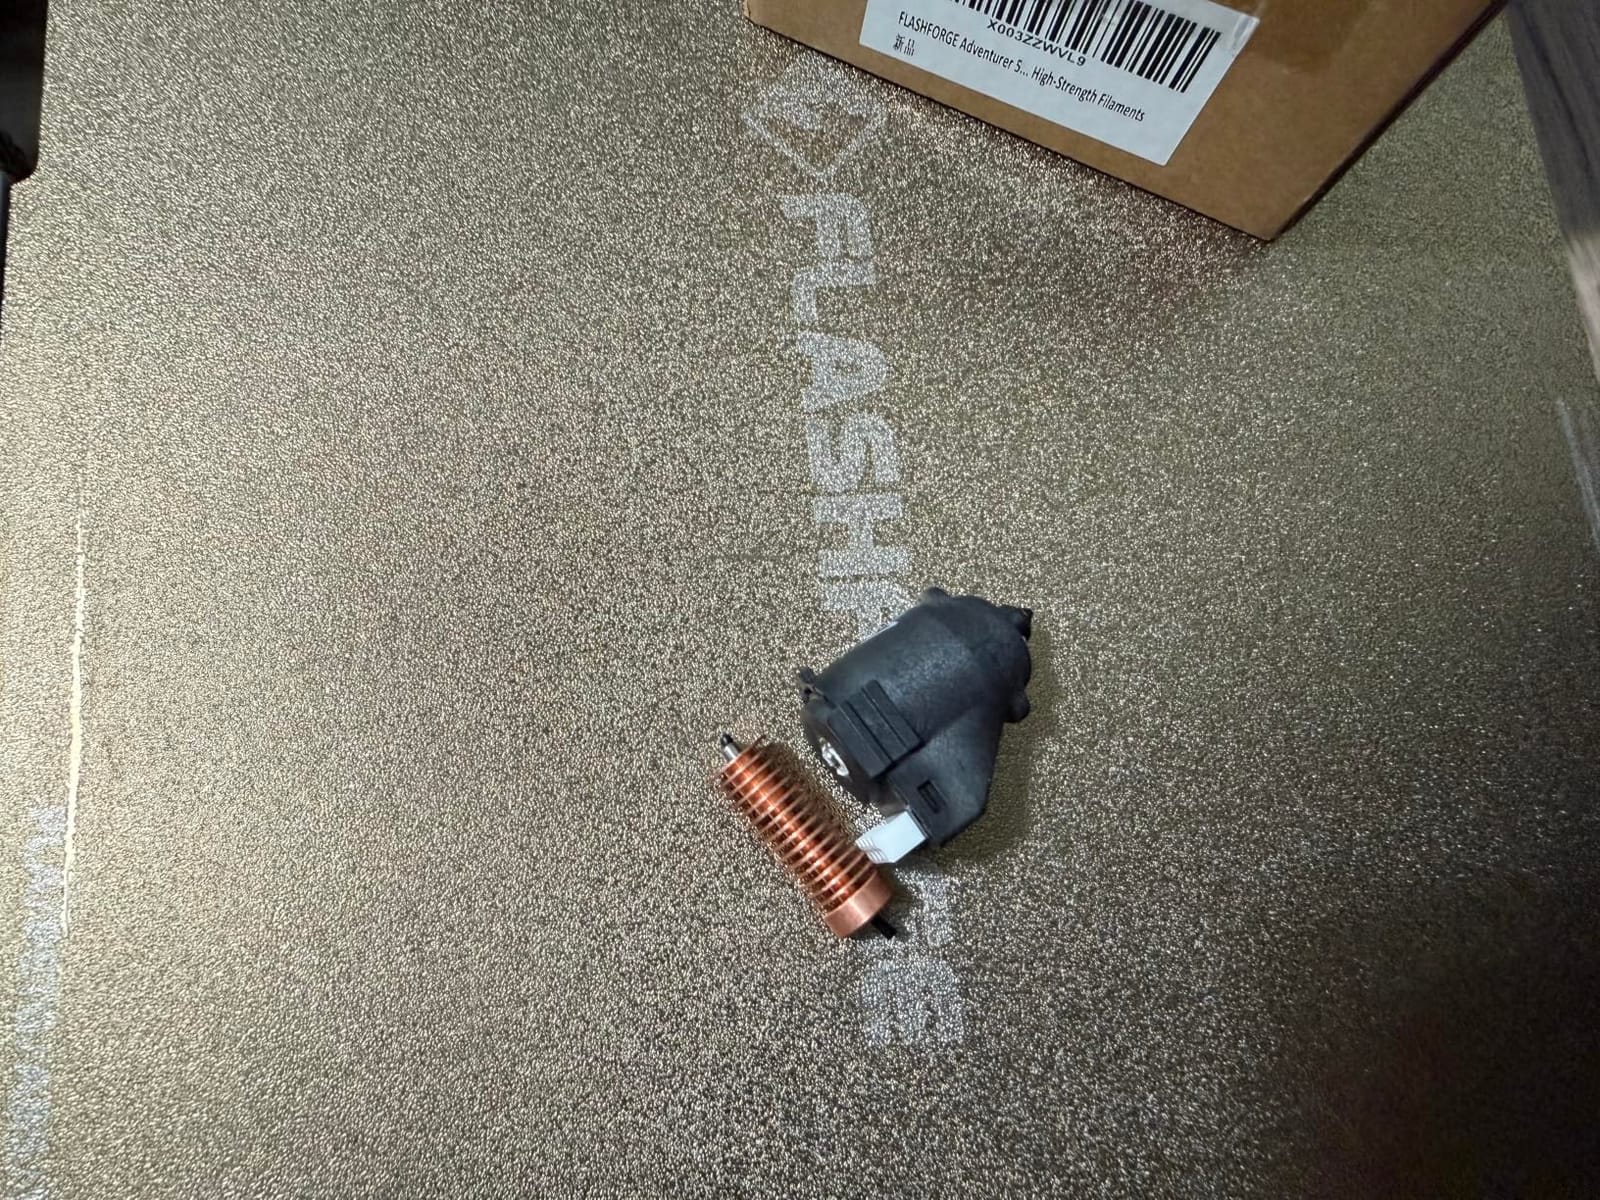
The tool-free quick release removes the nozzle in roughly three seconds, which is the feature that actually changes daily behaviour. Swapping between filament types stops being a fifteen-minute job with a wrench and a heat block cooling down, and that convenience compounds across a month of mixed printing.
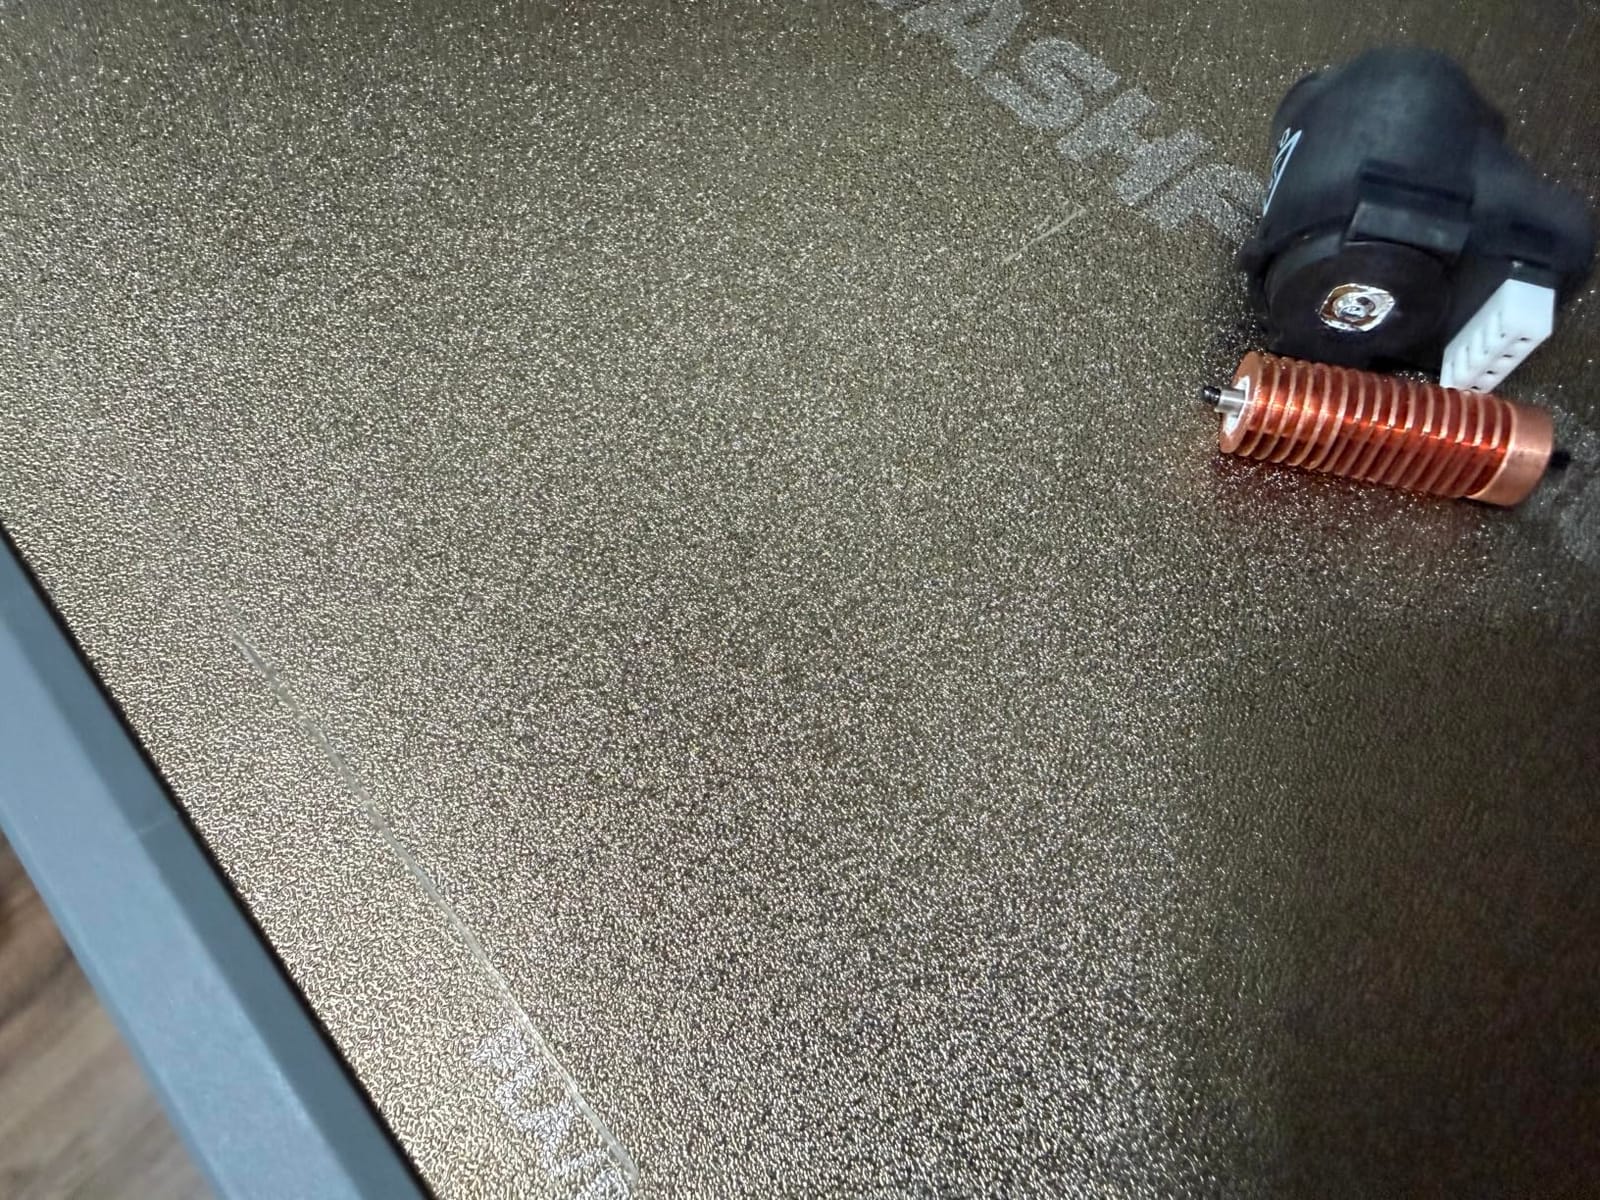
Owners report printing several kilograms of PA6-CF through a single 0.6 mm tip, which is a meaningfully different durability picture from the 0.4 mm steel options earlier in this guide. The reason is straightforward: a larger bore gives fiber bundles more room, so there is less contact pressure at the walls of the orifice. It also heats to 200°C in about 35 seconds.
The temperature ceiling is 280°C, which is the main limitation for this one. That covers PLA-CF, PETG-CF and most PA-CF work, but it is tighter than the OEM Bambu hotend and well below the tungsten carbide option further down. A 13 percent one-star share points to some quality variance between production runs.
Who should buy the Flashforge 0.6 mm nozzle
Buy it if you run a Flashforge Adventurer 5M or 5M Pro and you print carbon fiber in volume. The 0.6 mm bore and 32 mm3/s rating make it the best match on this list for big abrasive jobs where print time is the main cost.
It is also the right call if you have been fighting clogs on particle-filled filament at 0.4 mm. Moving up a bore size is often the cheapest fix there is, and this nozzle delivers that bore size from an official range rather than an aftermarket guess.
Who should skip it
Skip it if you need small features or thin walls, because a 0.6 mm bore will not hold fine detail. Skip it if you print PC-CF or anything needing more than 280°C, since the rating is the constraint rather than the material.
One owner reported the new nozzle being smashed into the build plate and damaging the extruder, which is a real handling risk with a tool-free quick release. If your Z-axis has any play, dial in the probe offset before you ever power the machine for the first time with this fitted.
6. Micro Swiss Plated Wear Resistant V6 0.4 mm – brass heat transfer with a wear coating
Microswiss Plated Wear Resistant Nozzle RepRap – M6 Thread 1.75mm V6 Compatible (.4mm)
- Keeps brass thermal conductivity under a wear coating
- Far less PETG sticking than bare brass
- Owners report 200-plus hours without clogs
- Made in the USA and available in five sizes
- Plating eventually wears through at the tip
- One owner reports it wore as fast as brass
- Costs more than a plain brass nozzle
- Thread can run long on some hexagon hotends
This is the clever middle path, and it exists because of the temperature problem rather than the wear problem. A brass core moves heat the way brass does, and the TwinClad XT plating adds a hard wear-resistant shell over it. You get the melt-zone behaviour of brass with more resistance to abrasion than plain brass provides.
That heat retention is why it holds a 4.6 average from 164 reviews. Owners on high-temperature prints report far less PETG sticking to the outside of the nozzle, and several describe running more than 200 hours and hundreds of print hours with no clogs at all. It fits all 1.75 mm V6 hotend printers including the Prusa i3 MK2, MK3 and Mini.
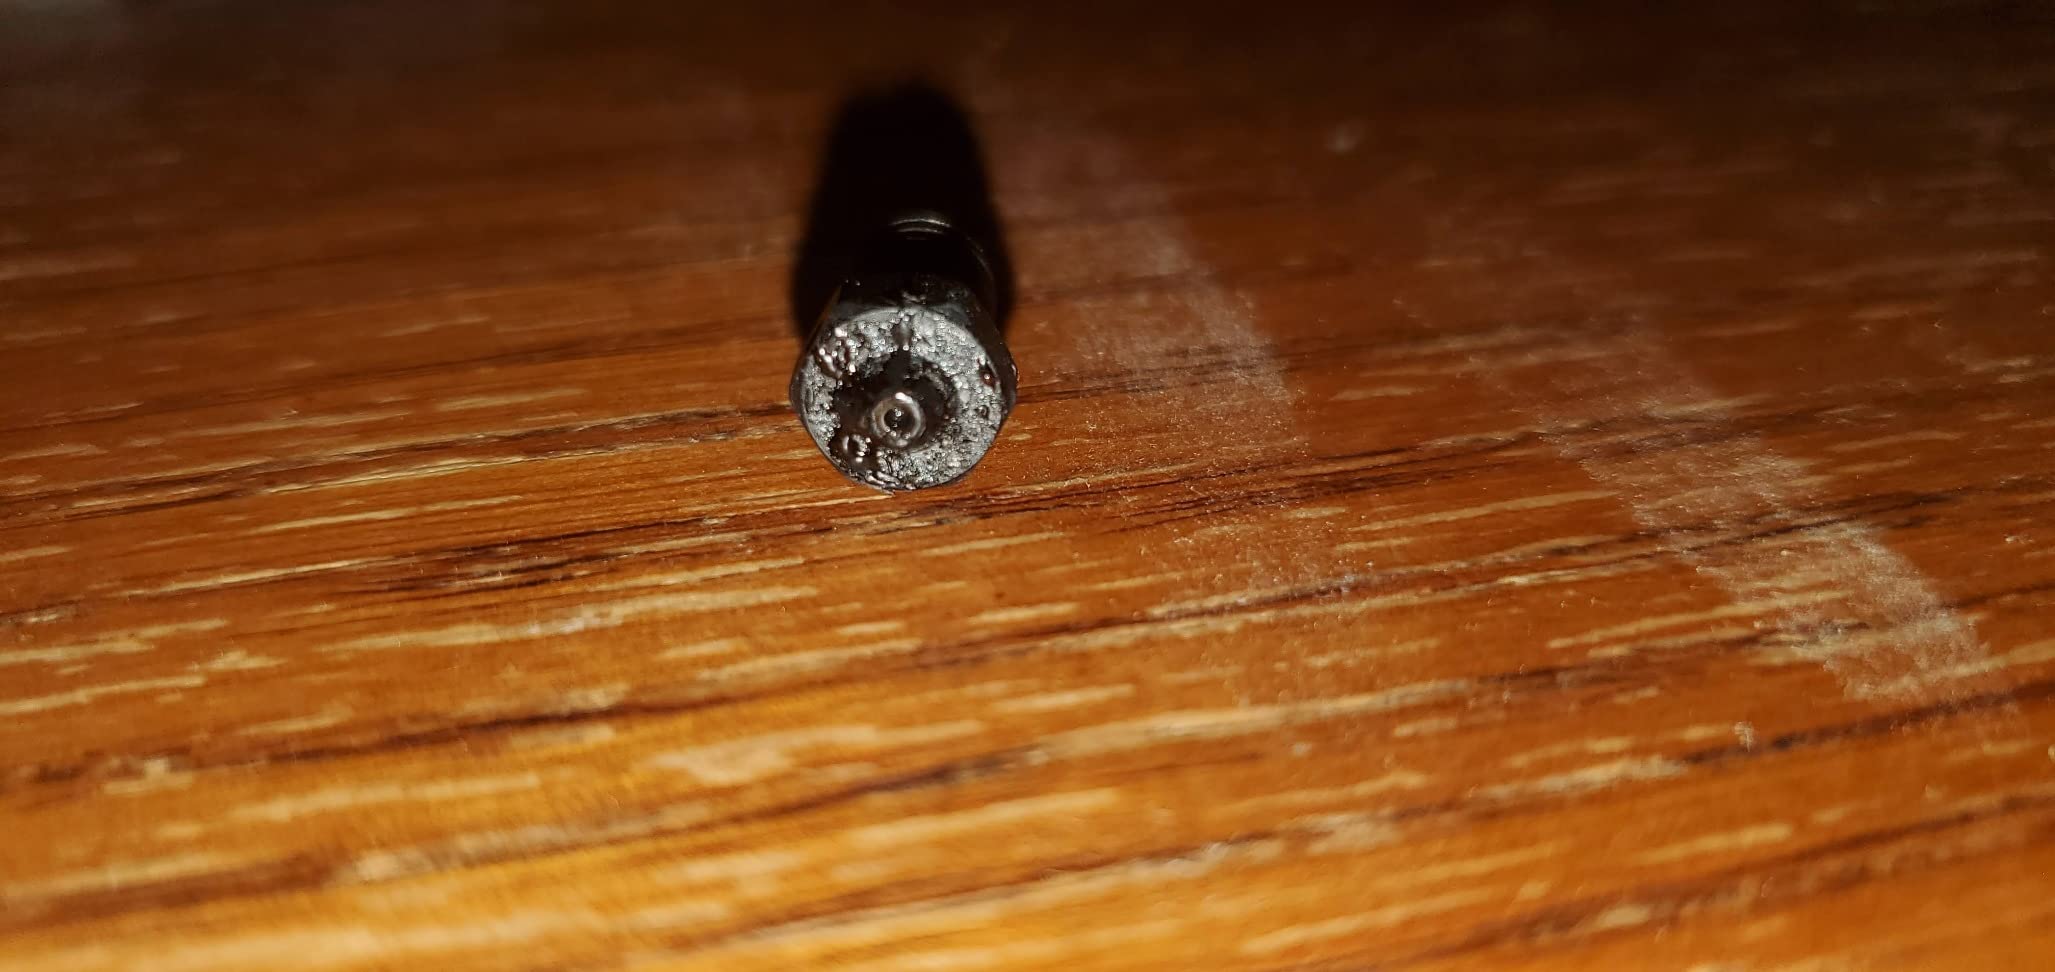
The honest limitation is that plating is a surface treatment, not a bulk material. It wears through at the tip eventually, typically after a year or more of use, and once it does the underlying brass is exposed. One owner reports the orifice opening from 0.25 mm to 0.5 mm, which is exactly the failure mode this design is meant to delay rather than prevent.
At 1 g and 3 by 2 by 0.5 inches it is a small, light part with a 6 mm inlet and a 0.4 mm outlet for standard 1.75 mm filament. It is made in the USA, and the range covers 0.25, 0.3, 0.4, 0.5 and 0.8 mm if you later want a different bore from the same design.
Who should buy the Micro Swiss plated nozzle
Buy it if you run a V6 hotend and you print carbon fiber occasionally but dislike raising temperatures every time you swap materials. The brass core means close to no temperature offset, which removes the most common surprise when moving to a steel-family tip.
It is also worth considering for PETG and general multi-material work where sticking and residue are the annoyance rather than abrasive wear. A 0.4 mm bore keeps standard resolution while the plating handles the odd CF print.
Who should skip it
Skip it if you print PA-CF or PPA-CF daily. Plating delays wear, it does not solve it, and a carbide or ruby tip will still be in service years from now. Skip it if the price premium over a plain brass nozzle bothers you, since several owners feel the performance gain does not justify it.
One more practical note: on some hexagon hotends the thread runs one to two turns long, so check that it bottoms out before you torque the heater block down. A nozzle that protrudes is a nozzle that leaks plastic around the threads.
7. LANKEGU Hardened Steel 0.4 mm Kobra 2 6-Pack – the budget per-tip pick
- Lowest cost per nozzle in the guide thanks to the six pack
- High-hardness steel with reasonable thermal behaviour
- Chamfered feed bore designed to reduce blockages
- Covers the whole Kobra 2 family
- Lowest average rating in the group at 4.0 with a 14 percent one-star share
- No written reviews were available to confirm long-term abrasive performance
The case for this one is arithmetic. Six tips at the lowest per-nozzle outlay of anything in this guide means a Kobra 2 owner can keep a genuine spare set on hand for very little, and a six-pack is also the easiest way to compare diameters or materials if you have never printed abrasives before.
The chamfered feed design is the detail worth noting. A chamfer at the entry to the bore reduces the angle at which filament first meets the wall, which lowers feed resistance and reduces the chance of a fiber bundle snagging at the entry point. The stated burr-free inner wall with a low viscosity coefficient is aimed squarely at the clog complaints that dominate this product category.
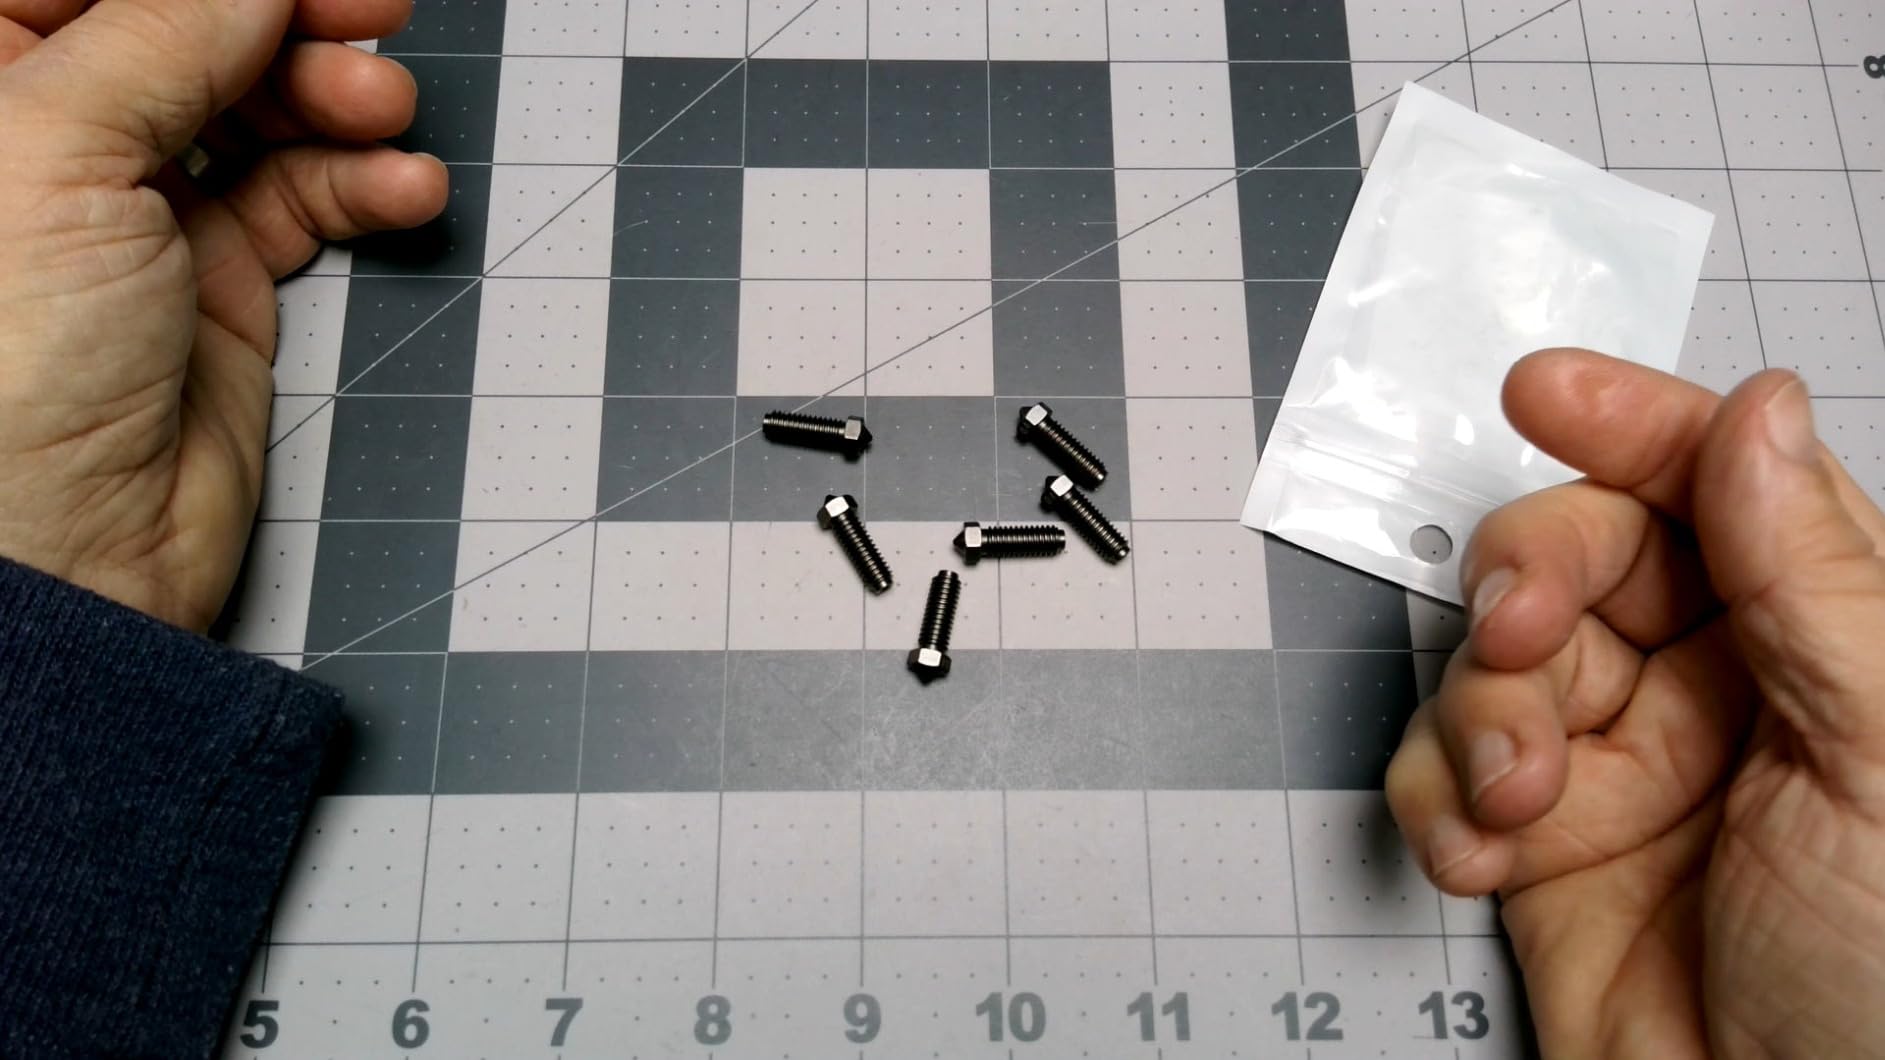
Fitment covers the Anycubic Kobra 2, 2 Neo, 2 Pro, 2 Plus and 2 Max, which is a broad family for one nozzle. It is listed as compatible with PLA, ABS, PETG, TPE, TPU and PC filaments, and at 0.4 mm bore it handles carbon fiber blends without the clogging pressure that a narrow bore creates.
We are flagging the evidence gap plainly. The 4.0 average from 68 reviews is the lowest in the group, with a 14 percent one-star share, and no written customer review text was returned in the data we worked from. That means the case rests on the spec sheet and the pack economics rather than on a body of owner experience, which is exactly why we put it at budget rather than above it.
Who should buy the LANKEGU Kobra 2 pack
Buy it if you own a Kobra 2 family machine and you want hardened steel capability with enough spares to stop worrying. The six-piece pack is genuinely the cheapest way to cover a year of occasional CF printing without thinking about it.
It is also a reasonable first abrasive nozzle for anyone who wants to test whether carbon fiber suits their workflow before investing in a carbide or ruby tip. The downside risk is a nozzle change rather than a project change.
Who should skip it
Skip it if you print PA-CF or higher-temperature blends as a primary material, because the rating and the evidence base are both modest. Skip it if you want confidence, since there is very little written owner feedback to lean on beyond the aggregate score.
Skip it entirely if you do not run a Kobra 2 machine. The fitment is specific to that family and there is no adapter that will make a different hotend accept it. Check your printer model before anything else, because that is the single most common reason a carbon fiber nozzle ends up unused.
8. POLISI3D Spider Hotend Hardened 0.4 mm 2-Pack – for Creality Spider machines only
- Hardened tool steel rated to 450°C for engineering plastics
- Two-pack covers the current tip and an immediate spare
- Centred and burr-free bore for smooth filament travel
- Fits only Spider-hotend Creality machines
- Small 71-review pool means limited durability data
- Will not fit Ender 3 models without the Spider hotend
The 450°C rating is the headline here, and it is genuinely unusual for a hardened steel nozzle at this level. That opens up PEEK and other engineering plastics alongside carbon fiber, which the 280°C and 300°C options elsewhere in this guide cannot reach. If you print CF in a material family that runs hot, this is the steel option that keeps up.
Fitment is narrow and worth stating twice. It is for Creality machines with the Spider high-speed hotend, covering the Ender 3 V3 SE, the Ender 3 V3 KE, the Ender 7 and the Ender 5 S1. It will not fit earlier Ender 3 models that do not have that hotend, which is the single most common mismatch people make on this platform.
The two-piece pack is simple and sensible. It gives you a spare for the moment the current tip wears through, and at 0.66 by 0.28 by 0.28 inches per tip the whole thing is small enough to lose in a drawer if you are not careful. The bore is described as round and centred for burr-free filament travel.
With 71 reviews at a 4.4 average, the owner history here is thin and no written review text was returned in our data. We are treating the material spec as the primary evidence. The 4.4 score is solid for what it is, but it is a smaller sample than most of the picks above and should be read that way.
Who should buy the Spider hotend nozzle
Buy it if you own an Ender 3 V3 SE, an Ender 3 V3 KE, an Ender 7 or an Ender 5 S1 and you print carbon fiber in combination with high-temperature engineering plastics. The 450°C rating is the reason to choose it over every other hardened steel option here.
It is a good match for a high-speed hotend in general, since Spider-based machines are built to push flow and a hardened tip holds its geometry better than brass under those conditions.
Who should skip it
Skip it if you run any Ender 3 without the Spider hotend, including the very common original Ender 3 and the Pro. The fitment is wrong and there is no way to make it work without replacing the hotend assembly, which defeats the purpose.
Skip it if you want the strongest evidence base. With 71 reviews and no written feedback available, you are buying on spec. For occasional CF work, the MK8 or V6 packs with a much deeper owner history are the safer bet if the hotend format allows it.
9. Dawnblade Tungsten Carbide MK8 0.4 mm – the hardest drop-in tip in the list
Tungsten Carbide MK8 Nozzle 0.4mm/1.75mm, Wear Resistant for 3D Printer
- 9 Mohs hardness matched to ruby and far above hardened steel
- 130 W/m·k conductivity is the highest in the guide
- 550°C rating covers PEEK-class materials
- Low 4.5 μm/m·°C expansion resists deformation on long prints
- No written customer reviews were returned to validate the claims
- Small 81-review pool with a 10 percent one-star share
- Second-highest outlay in the guide
Hardness is the headline, and the number is worth sitting with. The stated 9 Mohs matches ruby and sits far above hardened steel, which means the orifice resists abrasion at a level brass can only approach by being replaced. For a machine that eats nylon loaded with fiber every week, that is the difference between a consumable and a part.
The more interesting figure is the thermal one. A stated 130 W/m·k is the highest conductivity in this guide, compared with 45 for ruby and about 26 for hardened steel, and that is the opposite of the usual steel penalty. A carbide tip that moves heat into the melt zone faster means the polymer softens sooner and the nozzle can sustain higher volumetric flow without stalling.
The 550°C rating covers PEEK and other high-temperature engineering plastics, and the low thermal expansion of 4.5 μm/m·°C is the property that keeps it from deforming on long hot prints and large molds. It is nickel finished and fits the MK8 hotend of Ender and CR series machines, the CR-10 all-metal, the Prusa i3, the Anet A8 and Reprap.
We want to be direct about the evidence. The data returned 81 reviews at a 4.3 with a 10 percent one-star share, and no written review text came back, so the durability picture rests on the manufacturer specifications rather than on owner accounts. Those specs are unusually specific, which is a point in their favour, but it is not the same as a year of reported use.
Who should buy the tungsten carbide MK8 nozzle
Buy it if you run an MK8 machine and you print PA-CF, PA6-CF, PAHT-CF or PPA-CF as a routine material. This is the pick for the user who is already past worrying about wear and wants a tip that keeps its geometry indefinitely.
It also makes sense for mixed high-temperature work. The 550°C rating and the 130 W/m·k conductivity together mean one nozzle can cover nylon, CF nylon and PEEK-class materials without the temperature compromise that a steel tip imposes.
Who should skip it
Skip it if you print carbon fiber occasionally. The hardness advantage is real but you will not amortise it, and a hardened steel pack would cover the same use case. Skip it if you run a V6, Bambu, Creality Spider, QIDI or Flashforge, because the MK8 thread is specific.
Carbide tips are also brittle compared with steel. A bed crash, a Z-axis misalignment or a nozzle that gouges the build plate can chip an insert that is expensive to replace, and unlike a steel tip it cannot simply be filed back into shape. Handle it like a component that matters.
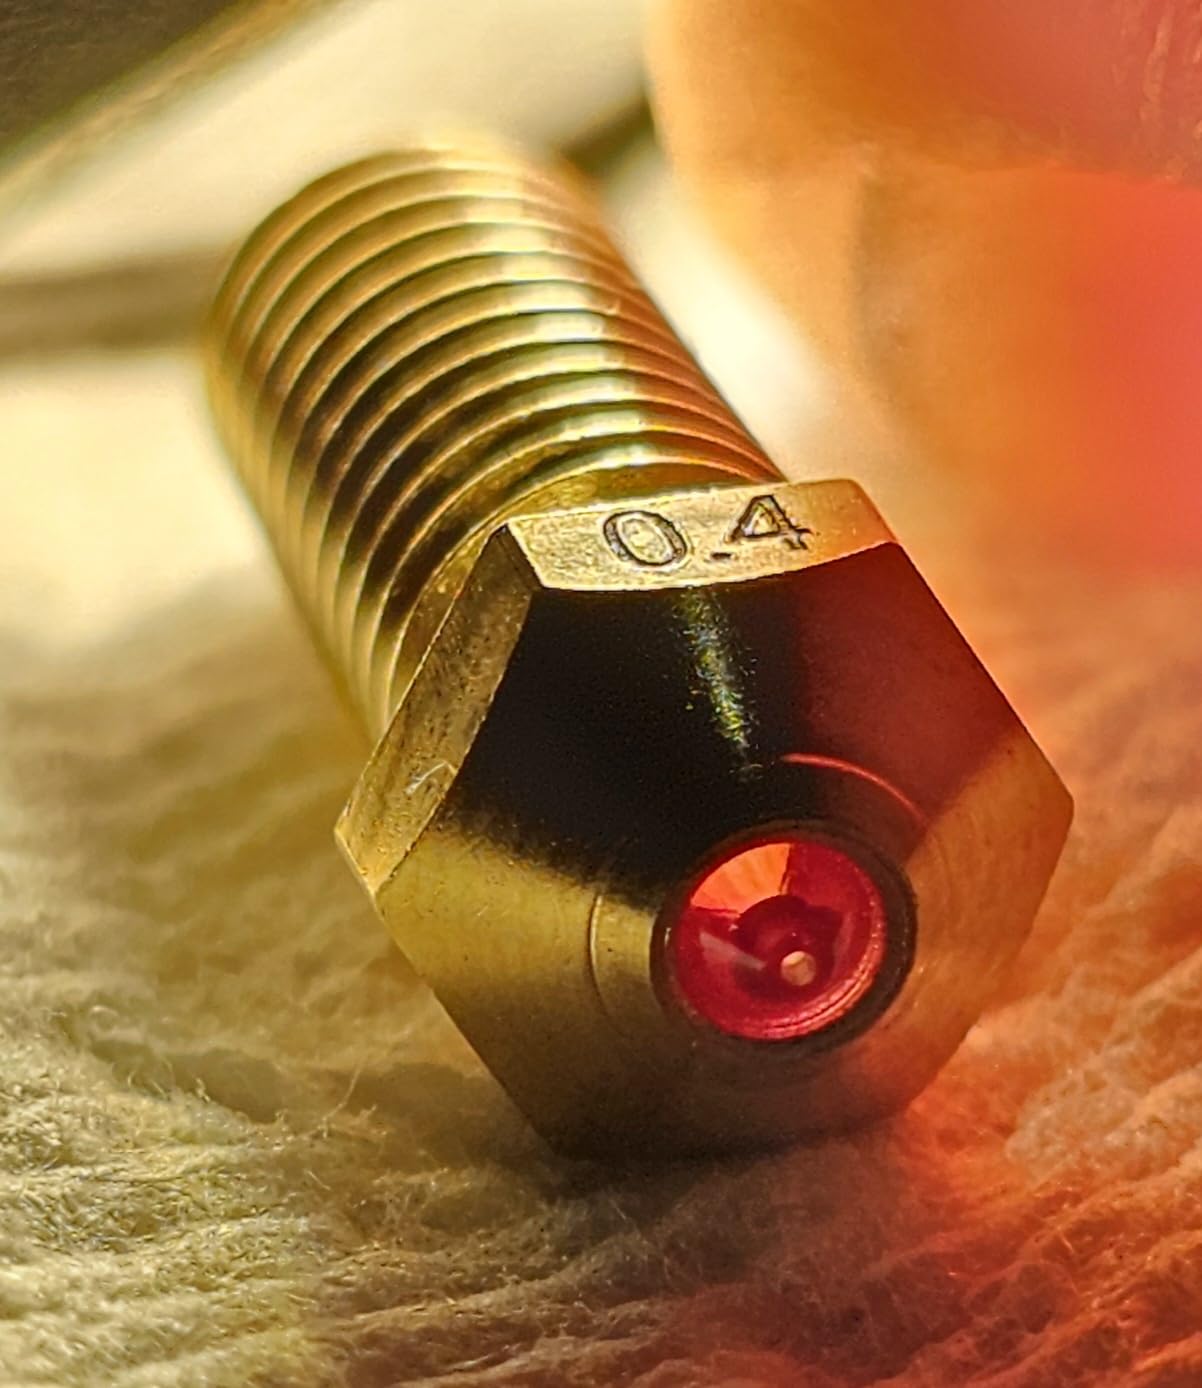
10. DUROZZLE Ruby 0.8 mm for QIDI Q1-Pro – real ruby in a nickel-plated copper body
- 84 percent five-star share is the strongest distribution in the guide
- Genuine ruby is the hardest common tip against fiber infill
- Nickel plating stops debris sticking and copper oxidation
- Funnel-shaped polished bore reduces carbonization
- No written customer reviews were returned
- 0.8 mm bore trades fine detail for throughput
The body material is what separates this from a cheap ruby insert. A sapphire tip is hard but conducts heat badly, so putting one in a brass body strands the benefit. Pairing it with a nickel-plated copper alloy body moves heat into the melt zone efficiently, which is what makes the ruby tip usable at print speeds rather than a curiosity.
The plating does three things at once according to the manufacturer. It is non-stick to debris so carbonized material does not weld itself to the outside, it hardens the surface, and it blocks copper oxidation. The funnel-shaped cut and polished bore avoids material accumulating in dead corners, which is the usual root cause of a blockage that no amount of cold pulling will clear.
Fitment covers the QIDI Q1-Pro, X-Max3, X-Smart3 and X-Plus3, and the range also includes ruby, tungsten carbide and diamond PCD tips at 0.4, 0.6 and 0.8 mm, so you can step down in diameter later without changing systems. At 0.882 ounces and 3.82 by 1.73 by 0.43 inches it is a compact drop-in.
It carries 81 reviews at 4.6 with an 84 percent five-star share, the strongest rating distribution among the picks here, though no written review text was returned. The 0.8 mm bore is the real trade-off: it suits abrasive and high-flow work rather than small precision parts, and it pairs naturally with the kind of large functional printing a QIDI X-Max3 or Q1-Pro is bought for.
Who should buy the DUROZZLE QIDI ruby nozzle
Buy it if you run a QIDI X-Max3, Q1-Pro, X-Smart3 or X-Plus3 and carbon fiber is a regular material. The 0.8 mm bore, the copper-alloy body and the funnel geometry are aimed squarely at throughput on abrasive filament.
It is also the option for anyone who wants a set-and-forget tip. Ruby does not wear in the way steel wears, so the replacement interval stops being something you have to think about between prints. The other tip materials in the same range let you keep the same body and change hardness if your material mix changes.
Who should skip it
Skip it if you print small precision parts, because a 0.8 mm bore cannot hold fine features or thin walls. Skip it if you run a different printer entirely; this is a QIDI-specific part and the mounting does not transfer.
And treat the tip as fragile. A ruby insert will chip from a bed crash, a crash-detection failure or a nozzle that has sunk into the build plate, and once the tip is chipped it is finished. Keep anti-seize on the threads, re-check Z-offset after any crash, and do not store tips touching tip to tip.
11. DUROZZLE Ruby 0.8 mm for Flashforge AD5X – ruby tip for chute-fed abrasive work
DUROZZLE Ruby Nozzle 0.8mm for Flashforge AD5X 3D Printer, Hardened & Abrasion Resistant for Precision Additive Manufacturing
- 82 percent five-star share across the review pool
- Ruby tip with nickel plating for long abrasive service
- Funnel geometry reduces carbonization and blockages
- Handles abrasive and standard PLA ABS and nylon
- 12 percent one-star share is the highest among the DUROZZLE picks
- No written customer reviews were returned
- 0.8 mm opening limits fine-detail work
The AD5X feeds material through a chute rather than a direct-drive gear, and that changes the wear picture. There is no drive gear grinding against the filament, so the nozzle is the sole abrasion surface in the path, which is exactly the situation a ruby tip is built for. If you run abrasive filament on this machine, this is the part that stops absorbing the damage.
Otherwise the design matches the QIDI ruby closely, and for the same reasons. A genuine sapphire tip sits in a nickel-plated copper body, the plating resists debris sticking and surface oxidation, and the polished funnel bore is cut to keep carbonized material from settling in dead corners where it would harden into a plug.
The rating is 4.4 from 49 reviews with an 82 percent five-star share, which is a strong profile for a relatively recent listing. The one-star share of 12 percent is the highest among the three DUROZZLE ruby nozzles, which is still a small number, but it is worth knowing before you commit to a single-format part.
It is built specifically for the Flashforge AD5X, and the wider range covers ruby, tungsten carbide and diamond PCD tips at 0.4, 0.6 and 0.8 mm. At 0.988 ounces and 3.54 by 2.36 by 1.02 inches it is a small part, and the same handling rules apply as for any ruby nozzle: anti-seize on threads, no tip-to-tip storage, and a crash check after any Z-axis fault.
Who should buy the AD5X ruby nozzle
Buy it if you own a Flashforge AD5X and you print carbon fiber, glass-infilled or metal-filled filament regularly. Chute-fed design means the nozzle takes the full abrasive load, and a ruby tip is the most wear-resistant option available for it.
It also suits anyone who wants to stop budgeting for nozzle replacements. The 0.8 mm bore is deliberate for this machine, matching the throughput the AD5X is built for rather than the fine detail of a smaller nozzle.
Who should skip it
Skip it if you need small parts or thin walls, since 0.8 mm rules those out. Skip it if you have any printer other than the AD5X, because this is a machine-specific part and the tip will not seat anywhere else.
Skip it if you are prone to crash-prone setups. The cost of a chipped ruby tip is much higher than a chipped steel tip, and no amount of cleaning will restore the edge. If your first-layer protection is unreliable, fix that before you fit a tip this hard.
12. DUROZZLE Quick-Swap Ruby 0.4 mm for Creality K2 – keeps 0.4 mm detail with ruby
- Keeps 0.4 mm detail while gaining ruby wear resistance
- Integrated all-metal nozzle and heat break swaps in seconds
- Nickel plating resists debris and oxidation
- Funnel-shaped polished bore reduces blockage
- 66 percent five-star share is the lowest of the three DUROZZLE picks
- No written customer reviews were returned
- Limited to the K2 family and Hi Combo
This is the one to look at if you want a ruby tip but do not want to give up 0.4 mm resolution. The other two DUROZZLE ruby nozzles here are 0.8 mm, which suits volume work. This one keeps the standard bore, so your layer height options and your fine feature capability stay where they were.
The integrated all-metal nozzle and heat break is the practical feature. Instead of a separate heat break and nozzle assembly, the two are one piece, so swapping takes seconds and there are no loose parts to lose. For anyone running multiple filaments on one machine, that changes how often you are willing to change over.
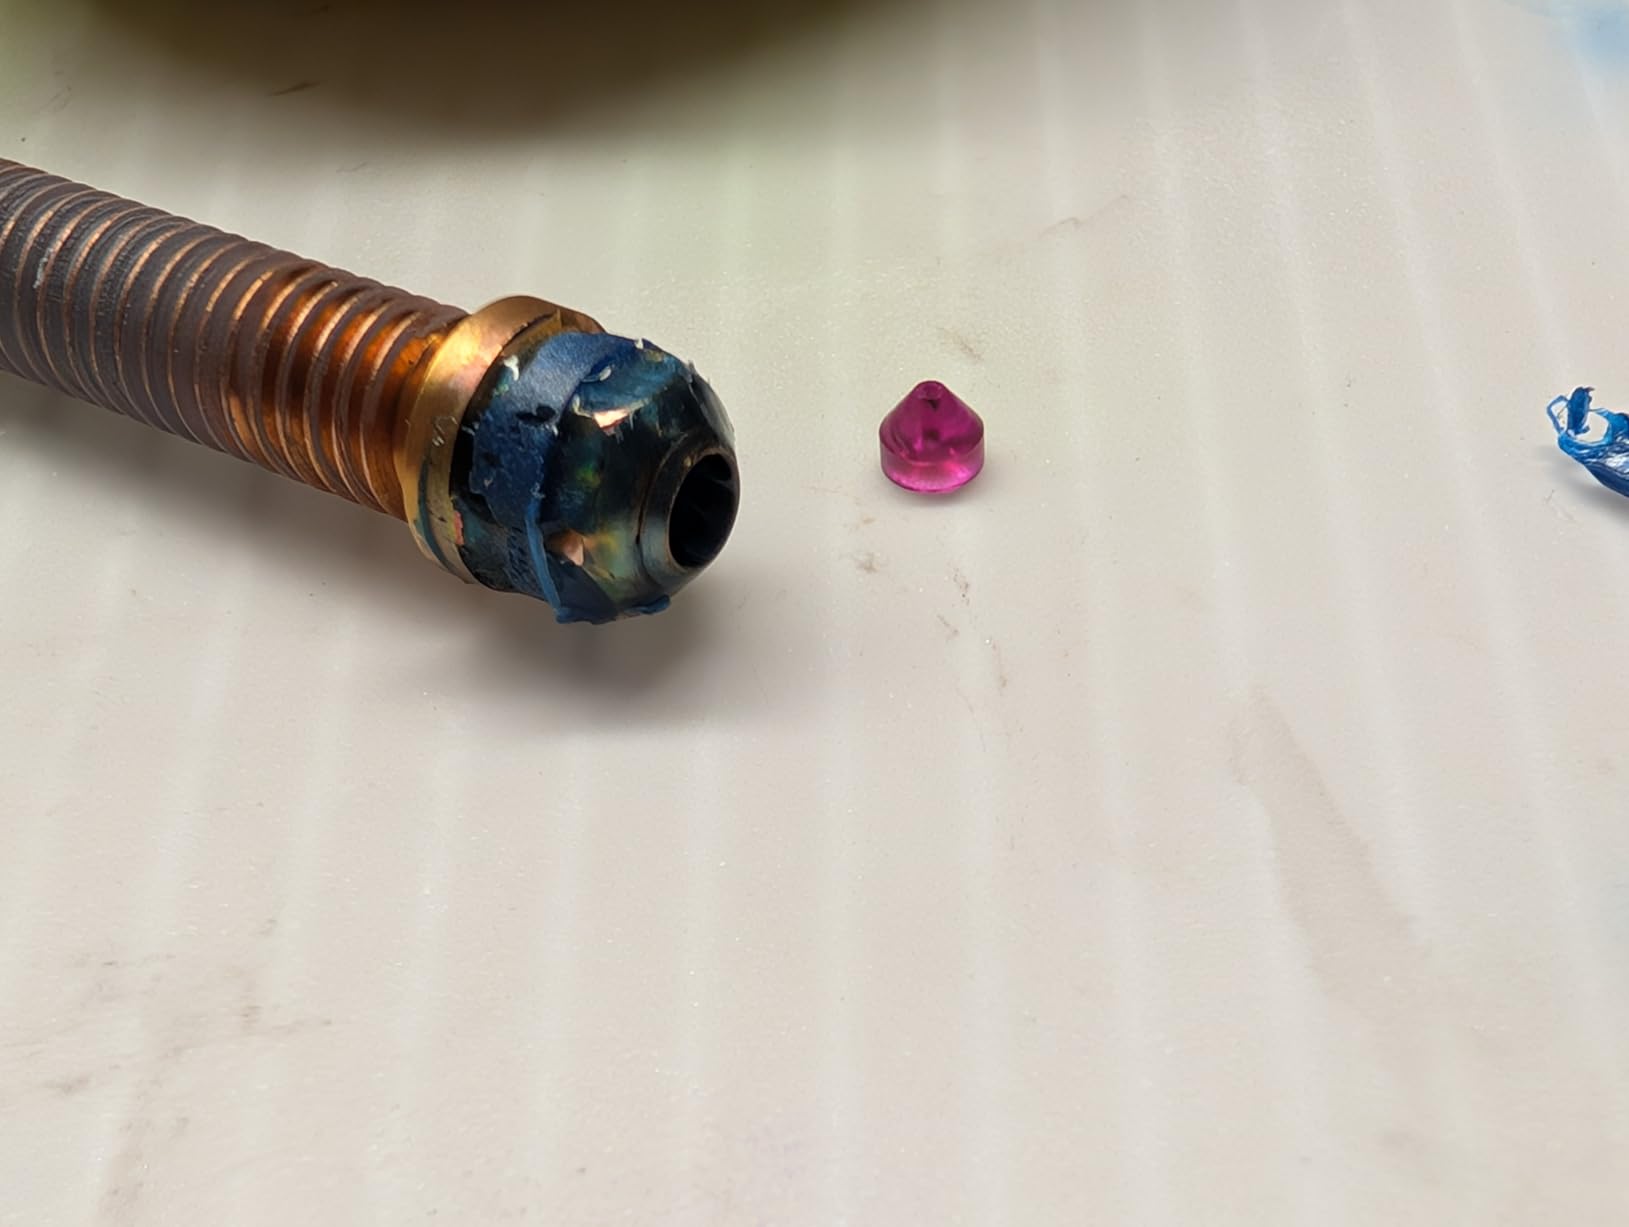
Fitment is for the Creality K2, K2 Plus, K2 Pro and the Hi Combo, and the same family also offers tungsten carbide and diamond PCD tips at 0.4, 0.6 and 0.8 mm. At 1.13 ounces and 3.7 by 1.73 by 0.47 inches it is the largest of the three ruby options in this guide by measurement, which reflects the integrated heat break.
The rating is 4.4 from 46 reviews with a 66 percent five-star share and a 26 percent four-star share. That is the most mixed distribution of the three DUROZZLE nozzles, with a few two-star reports in the mix. No written review text was returned, so we are reading the rating shape and the specification rather than owner accounts here.
Who should buy the K2 quick-swap ruby nozzle
Buy it if you own a K2, K2 Plus, K2 Pro or Hi Combo and you want both 0.4 mm detail and long service life under carbon fiber. It is the best balance of resolution and wear resistance among the ruby options here.
The quick-swap integrated design suits multi-material workflows, where swapping between abrasive and non-abrasive filament several times a week is normal. Everything else in the nozzle is aimed at the same goal: keeping the bore clean enough that you are not cold-pulling every week.
Who should skip it
Skip it if you print large functional parts where throughput matters more than detail, because the 0.8 mm options are the better tool for that. Skip it if you run any other Creality or another brand entirely, since this is a K2-family part only.
And consider the mixed five-star share before committing. With 46 reviews this is the smallest evidence base in the guide. If a large print job depends on it, run a short test first and keep your current nozzle installed until you are satisfied rather than committing the only tip you have.
Nozzle material explained: brass vs hardened steel vs tungsten carbide vs ruby
Nozzle selection comes down to two properties that pull in opposite directions. Hardness decides how long the orifice survives abrasive fiber. Thermal conductivity decides how well the melt zone keeps up with the flow your printer is asking for. Brass wins the second and loses the first badly, and most of the confusion in this category comes from people optimising one and ignoring the other.
Brass is soft and excellent at moving heat. That makes it the default because it handles temperature gracefully and costs almost nothing to replace, but carbon fiber strands are harder than the copper alloy that surrounds the hole, so the orifice enlarges. The enlargement is gradual, which is why the first symptom is usually a wall that measures slightly thick and a first layer that sits lower than expected.
Hardened steel fixes the wear problem and introduces a temperature one. It conducts roughly a quarter of the heat brass does, so the melt zone runs cooler than the heater block reading suggests, and prints underextrude until you add temperature. Members of the Prusa forum describe this compensation as a routine adjustment rather than a defect, and the Thingiverse engineering forum makes the same point about the heater reading being correct while the melt zone is not.
Coated brass exists to dodge that compromise. A hard plating over a brass core, which is what the Micro Swiss option in this guide uses, keeps the heat behaviour people like while adding meaningful abrasion resistance. It delays wear rather than eliminating it, because once the coating wears through at the tip the core is exposed.
Tungsten carbide inverts the usual problem. A carbide tip is extremely hard and, in the Dawnblade option here, rated at 130 W/m·k, which is higher than ruby. The cobalt binder in a carbide nozzle is the weak point in a different way: long acetone soaks can attack it, so cleaning should be mechanical, such as a brass brush or a cold pull, rather than chemical.
Ruby is synthetic sapphire and is the hardest common nozzle material. It is also chemically inert, so solvents pose no risk to the tip, and it resists abrasion better than carbide. The penalty is thermal: ruby conducts heat poorly compared with carbide, which is why the best ruby nozzles put the insert in a copper-alloy body rather than brass.
On longevity evidence, be sceptical of both extremes. Vendor claims of brass lasting only tens of hours on PA-CF sit alongside r/3Dprinting accounts of finishing an entire carbon fiber roll on an Ender 3 brass nozzle, and the Bambu community consensus is that all most people need is a hardened tip. The honest synthesis is that print temperature and duration drive wear far more than filament name does.
The longest longitudinal data point available comes from a ruby nozzle outside this roundup. A 3dpblog report describes a Trianglelab high-temperature ruby running over two years of daily service on a Voron hotend, printing PEEK at 450°C, and retired after three years when the tip edges went visibly irregular. That is the kind of time horizon you are buying when you move to a ruby tip.
Community recommendation on r/prusa3d favours ruby and carbide from Durozzle for multi-printer setups, with owners noting they run standard speed profiles fine despite not being high-flow designs. That counters the common assumption that a carbide or ruby tip forces you to slow everything down, and it matches the 0.8 mm throughput logic behind the ruby options in this guide.
Choosing nozzle diameter for carbon fiber: 0.4 vs 0.6 vs 0.8 mm
For carbon fiber, 0.6 mm is the better default if your printer supports it, and 0.4 mm if you need detail. A larger bore gives fiber bundles more clearance, lowers the contact pressure on the orifice wall and clogs far less often, and it also pushes more material per second which shortens print time. Stay on 0.4 mm for small features and thin walls, and avoid 0.2 mm entirely, because fiber strands catch in a hole that narrow.
The other common question is layer height. A workable rule is to keep layer height between 25 and 75 percent of your nozzle diameter. With a 0.6 mm bore that means 0.15 to 0.45 mm layers, which covers the entire useful range for most functional parts without asking the nozzle to do anything it cannot.
Going wider also changes the wear maths. A 0.6 mm nozzle running the same filament volume touches the orifice wall with less pressure than a 0.4 mm, and several owners of the Flashforge option in this guide report several kilograms of PA6-CF through a single tip. That is a different durability conversation from the 0.4 mm steel packs, and it is worth weighing before you commit.
Check your thread standard before you buy a carbon fiber nozzle
Confirm the thread standard first, because it is the number one reason a carbon fiber nozzle arrives and cannot be fitted. The MK8 screw-in covers most Creality Ender and CR series machines, the CR-10 all-metal, the Prusa i3, the Anet A8 and Reprap. The V6 and M6 thread covers E3D V6 derivative hotends, the Prusa i3 MK3 and MK3S, the Prusa Mini and the Anycubic Mega.
Everything else on this list is machine-specific. Bambu uses a quick-swap hotend with a threaded nozzle, split between the A1 family and A2L on one side and the P1S, P1P and X1C on the other. Creality Spider hotends use their own mounting, and the QIDI and Flashforge ruby options fit only the named models.
If you are unsure, remove the existing nozzle and look at the thread. Count the thread diameter visually against a known M6 part, or check the hotend model in your printer documentation. Forums fill with owners who assumed MK8 fit a V6 printer and discovered otherwise mid-project, and five minutes of checking prevents that entirely.
Check the temperature rating against your filament at the same time. The options here range from 280°C to 550°C, and the higher-temperature ones give you room to run PEEK and PEI alongside carbon fiber. A nozzle that meets your needs for PLA-CF may not be the one you want when you move to PC-CF next year.
How to tell a worn nozzle and when to replace it
Four symptoms point to a worn nozzle. Walls that measure thicker than your slicer setting, stringing that appears from the nozzle even with retraction tuned, a first layer that is visibly squashed or uneven, and dimensional drift where printed parts no longer fit their slots. All four are caused by the same thing: a hole that has grown past its nominal diameter.
To check, pull the nozzle and pass a 0.4 mm cleaning pin through the orifice. If it drags heavily or will not pass, the opening is already enlarged. For a more precise reading, a pin gauge set or calipers on the tip can give you a usable figure, and comparing against a new nozzle tells you how far it has worn.
Replace rather than drill. Widening a hole with a pin or a drill does not restore the geometry, and the walls of the drilled hole are rougher than the original bore, which increases both wear rate and clogging. A new tip is a small part and a short print to replace.
On intervals, be guided by the material rather than the calendar. Steel tips on PLA-CF and PETG-CF generally last longer because the abrasive load and temperature are lower. Steel on PA-CF, PA6-CF or PPA-CF wears considerably faster, which is the point at which carbide or ruby becomes the sensible upgrade. Carbonized residue around the outside of the tip is a separate signal, because it means a cold pull has been overdue.
Installing a carbon fiber nozzle without damaging it or your hotend
Start cold where your hotend allows it, and put a thin layer of anti-seize or boron nitride paste on the threads before you screw the nozzle in. Steel and carbide threads will gall against an aluminum heater block, and a seized nozzle can damage the block when you try to remove it. Paste costs nothing and prevents most of the headaches reported on the Prusa and Bambu forums.
Do not hot-tighten. Snug is enough, and over-torquing a steel or carbide nozzle into an aluminum block cracks the block rather than securing the nozzle. If the nozzle protrudes below the heater block when you are done, it is not seated properly and plastic will leak around the threads instead of through the orifice.
After any nozzle change, add temperature. Moving from brass to steel, tungsten carbide or ruby typically needs 5 to 15 degrees more at the nozzle, because the melt zone runs cooler even though the heater block reading looks correct. Then run a PID autotune, since the thermal mass and the response curve of the new nozzle are different from what the controller was tuned against.
Finish with a temperature tower and a single-wall test so you can see the flow rate directly. If the line is thinner than expected, add temperature; if it is thicker, subtract. Doing this once after every nozzle change is what prevents the underextrusion complaint that makes people think their carbon fiber nozzle is faulty.
On cleaning and storage, match the method to the tip. A cold pull and a brass brush work for steel and carbide, and long acetone soaks are the wrong choice for carbide because of the cobalt binder. Ruby is solvent-proof, so chemical cleaning is not a concern. Never store hardened or ruby tips touching tip to tip, and do not tighten a hot nozzle against a cold block.
Frequently Asked Questions
What nozzle do I need for PLA CF?
A hardened steel nozzle is the right choice for PLA-CF and PETG-CF. These filaments carry a lower abrasive load and print cooler than nylon blends, so hardened tool steel in a 0.4 mm bore handles them without the temperature offset that a carbide or ruby tip would need. Step up to tungsten carbide or a ruby tip in a copper-alloy body only if you move to PA-CF, PA6-CF or PPA-CF as a daily material.
Is a hardened steel nozzle better than brass?
Yes, for any abrasive filament. Carbon fiber strands are harder than brass and wear the orifice open within a few prints, which causes over-extrusion, stringing and parts that drift out of tolerance. Hardened steel resists that wear far better. The trade-off is thermal, since steel conducts heat poorly compared with brass, so you typically add 5 to 15 degrees and re-tune PID after fitting one.
Is .6 or .4 nozzle better?
For carbon fiber, 0.6 mm is better when your printer supports it, because the wider bore gives fiber bundles more clearance and clogs far less often. Choose 0.4 mm when you need small features or thin walls. Avoid 0.2 mm with carbon fiber, since fiber strands catch in an opening that narrow. A useful rule is to keep layer height between 25 and 75 percent of the nozzle diameter.
Is a tungsten carbide nozzle better than hardened steel?
For regular PA-CF or PPA-CF printing, yes. A tungsten carbide tip is rated at 9 Mohs hardness, far above hardened steel, and resists abrasion at a level steel cannot match. It also conducts heat better than steel in the Dawnblade option in this guide, at a stated 130 W/m·k, so it can sustain higher flow. The trade-offs are cost, brittleness and the fact that a chipped carbide tip cannot be filed back.
Are ruby nozzles worth it?
Ruby is worth it if carbon fiber is a regular material on your machine and you print functional or tooling parts. A genuine ruby tip is the hardest common nozzle material and is chemically inert, so it resists abrasion and solvents better than carbide. Put the insert in a copper-alloy body, because ruby conducts heat poorly on its own. For occasional PLA-CF work, a hardened steel nozzle is the sensible choice instead.
What are the downsides of using hardened steel nozzles?
The main drawback is thermal conductivity. Steel moves heat far worse than brass, so the melt zone runs cooler than the heater block reading shows and prints underextrude until you add 5 to 15 degrees. Steel is also harder than brass, so it galls against aluminum heater blocks and needs anti-seize on the threads. Finally, it still wears under heavy abrasive load, so PA-CF and PPA-CF work will eventually justify a carbide or ruby upgrade.
Conclusion: the best 3d printer nozzles for carbon fiber filament in 2026
Start with the Mudder hardened steel 0.4 mm MK8 pack if you run an Ender, a CR-10 or a Prusa i3 and carbon fiber is an occasional material. It has the deepest owner history in the guide, a bore that stays round, and ten tips so an error costs you nothing.
If you own a Bambu machine, take the OEM hardened hotend for the P1S, P1P and X1C, or the quick-swap hardened kit for the A1 family. If you run a Flashforge Adventurer 5M or 5M Pro, the 0.6 mm high-flow hardened nozzle cuts print time and clogs. For V6 hotends, the POLISI3D set or the Micro Swiss plated nozzle both work, depending on whether you want a spare pack or better heat transfer.
When carbon fiber becomes a daily material, move up. Tungsten carbide in a MK8 hotend and ruby tips in copper-alloy bodies for QIDI, Flashforge and Creality K2 machines are the picks for users who would rather stop replacing parts. Whichever you choose, confirm the thread before you order, add temperature after fitting, and re-tune PID before you blame the filament.